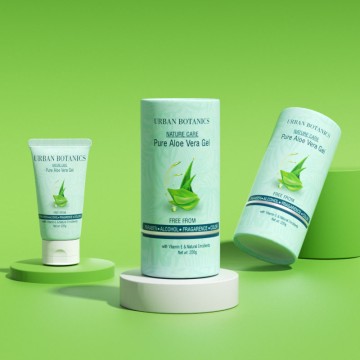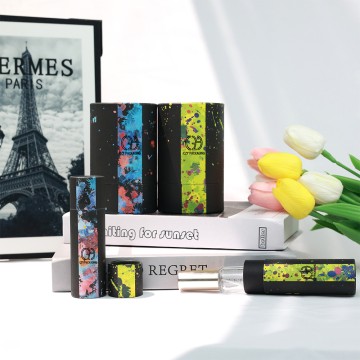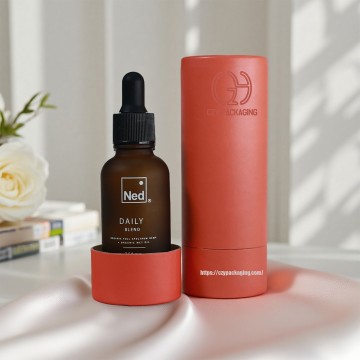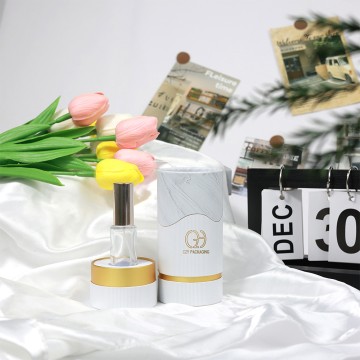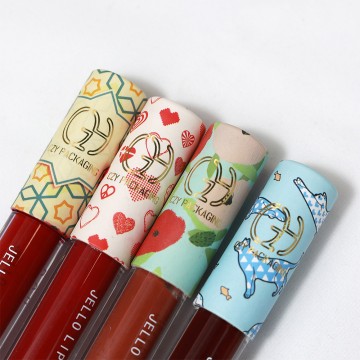
 Cosmetics
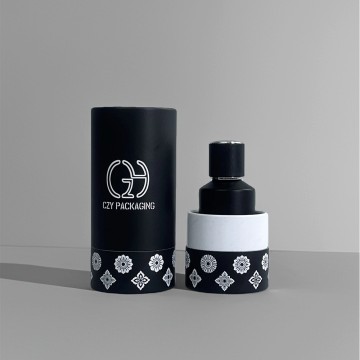
 Perfume, Essential Oil
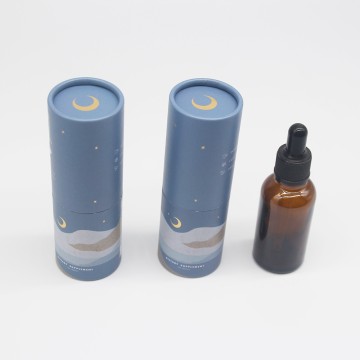
 Daily Necessities
 Food Paper Tube
 Personal Care
 Paper Bag
 Paper Box
Leave Your Message
Discover our top-tier paper tube and airplane box designs, meticulously crafted for New Zealand's thriving cosmetics, skincare, and fragrance markets. Engineered for durability during transit across the North and South Islands.
New Zealand, globally recognized for its pristine landscapes and rigorous environmental commitments, is undergoing a massive transformation in its commercial packaging sector. As a premium Airplane Paper Box Manufacturer & Factory catering to the New Zealand market, we understand that modern packaging must transcend basic functionality. Today, an airplane box (often referred to as a mailer box) serves as the primary physical touchpoint between e-commerce brands and Kiwi consumers, stretching from the bustling urban centers of Auckland and Wellington to the remote rural addresses of the South Island.
The local industrial status of paper packaging in New Zealand is heavily influenced by the nation's robust agricultural export market and its rapidly expanding domestic e-commerce ecosystem. High-value exports such as Manuka honey, premium dairy products, boutique wines from Marlborough, and organic skincare require packaging that guarantees structural integrity during long-haul international aviation transit, while simultaneously projecting a luxury, eco-conscious brand image. This dual requirement has driven the demand for highly engineered, corrugated airplane paper boxes that offer superior crush resistance without the weight penalty that inflates air freight costs.
Furthermore, the integration of AI technology in structural design is revolutionizing how these boxes are manufactured. Through advanced algorithms, we can simulate stress tests and optimize the die-cut patterns of airplane boxes, reducing material waste by up to 15% while enhancing the load-bearing capacity. This tech-driven approach ensures that every cubic centimeter of cargo space is utilized efficiently, a critical factor for New Zealand exporters reliant on global aviation logistics networks.
Aligning with New Zealand's ambitious goal to reach net-zero carbon emissions by 2050, the packaging industry is experiencing a definitive shift towards a circular economy. The traditional unboxing experience is being redefined by 100% recyclable, compostable, and biodegradable materials. Airplane paper boxes manufactured for the NZ market now frequently utilize FSC-certified virgin pulp and recycled plant fibers. Water-based, soy-derived inks and food-grade eco-friendly adhesives have replaced toxic chemical alternatives, ensuring that the packaging can be safely composted in a standard Kiwi backyard or processed by municipal recycling facilities without leaving harmful microplastics or chemical residues.
In the domestic market, localized application scenarios are vast. Boutique fashion labels in Christchurch, artisanal coffee roasters in Hamilton, and indigenous Maori health and wellness brands are increasingly adopting custom-printed airplane boxes. These boxes act as a mobile billboard. Advanced printing technologies, including ICC color management systems, allow for the precise reproduction of intricate "Kiwiana" motifs—such as the Silver Fern or intricate Koru patterns—enhancing the unboxing experience. The structural design of the airplane box, featuring secure locking tabs and double-walled sides, is specifically tailored to withstand the rigors of the NZ Post courier network, ensuring products arrive in pristine condition.
The future trend points unequivocally towards Smart Packaging. By integrating QR codes, NFC tags, and augmented reality (AR) markers directly onto the surface of the airplane paper boxes, brands can offer New Zealand consumers a highly interactive experience. A customer receiving a skincare product can scan the box to verify its authenticity, trace the origin of the botanical ingredients back to a specific farm in Rotorua, and receive personalized usage instructions via an AI-driven digital interface. This convergence of physical paper manufacturing and digital tech is setting a new benchmark for premium packaging.
Merging global manufacturing excellence with localized New Zealand market insights, we provide unmatched quality, customization, and sustainability.
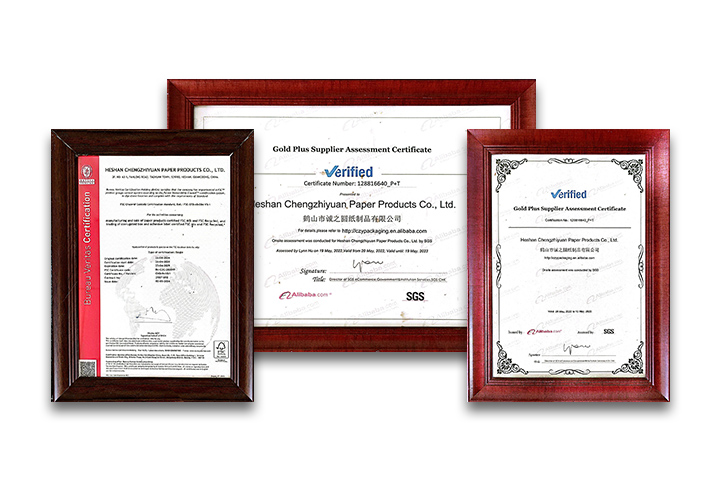
We have established a comprehensive quality management system, fully compliant with ISO 9001 quality management system and FSC certification for sustainable materials. For food-contact packaging, which is vital for New Zealand's agricultural and health exports, we strictly follow GB 4806.8-2022, EU REACH, and FDA standards, passing SGS, ITS, TUV, and BV third-party inspections. This ensures every airplane box meets the highest global safety protocols.
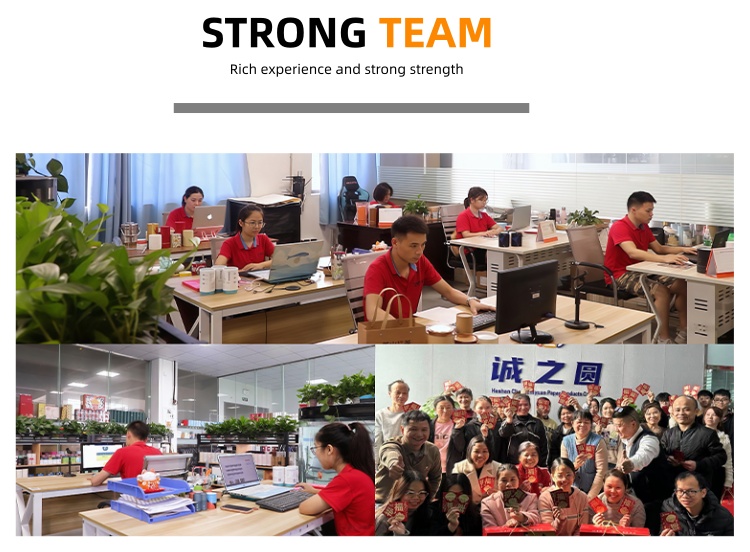
Our professional R&D and design team provides end-to-end customization from concept design to mass production. We offer an ICC color management system to control color difference ΔE within 1.5, ensuring consistent color reproduction across samples and bulk production. Advanced post-processing techniques include hot stamping, cold foiling, embossing, debossing, UV spot varnishing, leather texture pressing, and matte lamination to enhance brand premiumness. We support low MOQ for market testing and flexible production for both small-batch customization (from 500pcs) and large-batch orders (100,000+pcs), with sample delivery in 3-7 days and bulk production lead time of 2-4 weeks.
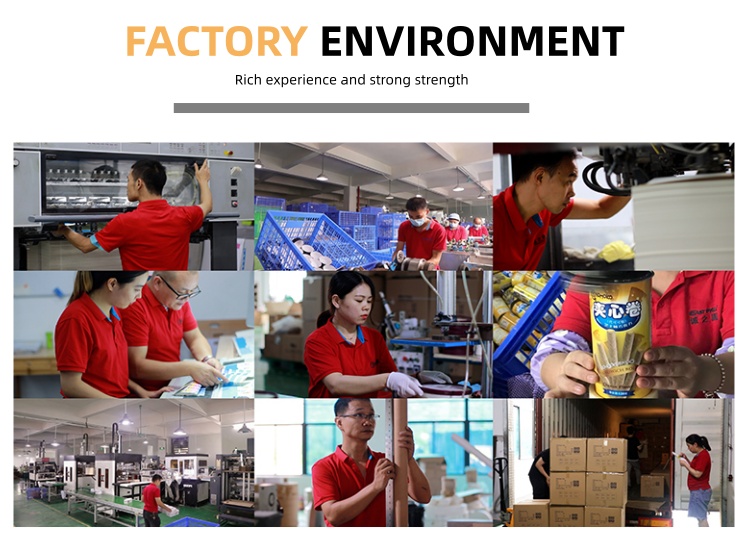
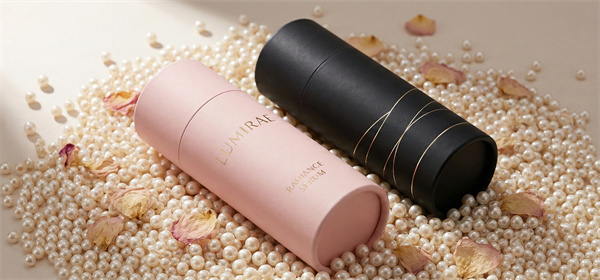
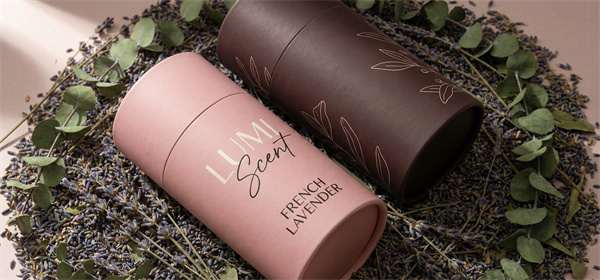
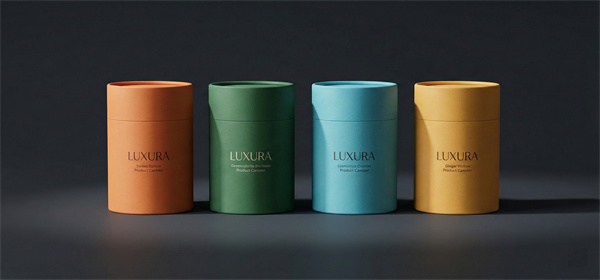
Committed to green packaging development, we adopt 100% recyclable, compostable, and biodegradable materials, including FSC-certified virgin pulp, recycled plant fiber paper, and food-grade eco-friendly adhesives. Our Eco-Push® series paper tubes and folding airplane boxes are designed as sustainable alternatives to single-use plastic packaging, widely used in solid cosmetics and personal care products. We strictly control production processes to reduce our carbon footprint, meeting the strict environmental responsibility requirements of New Zealand and global brands.
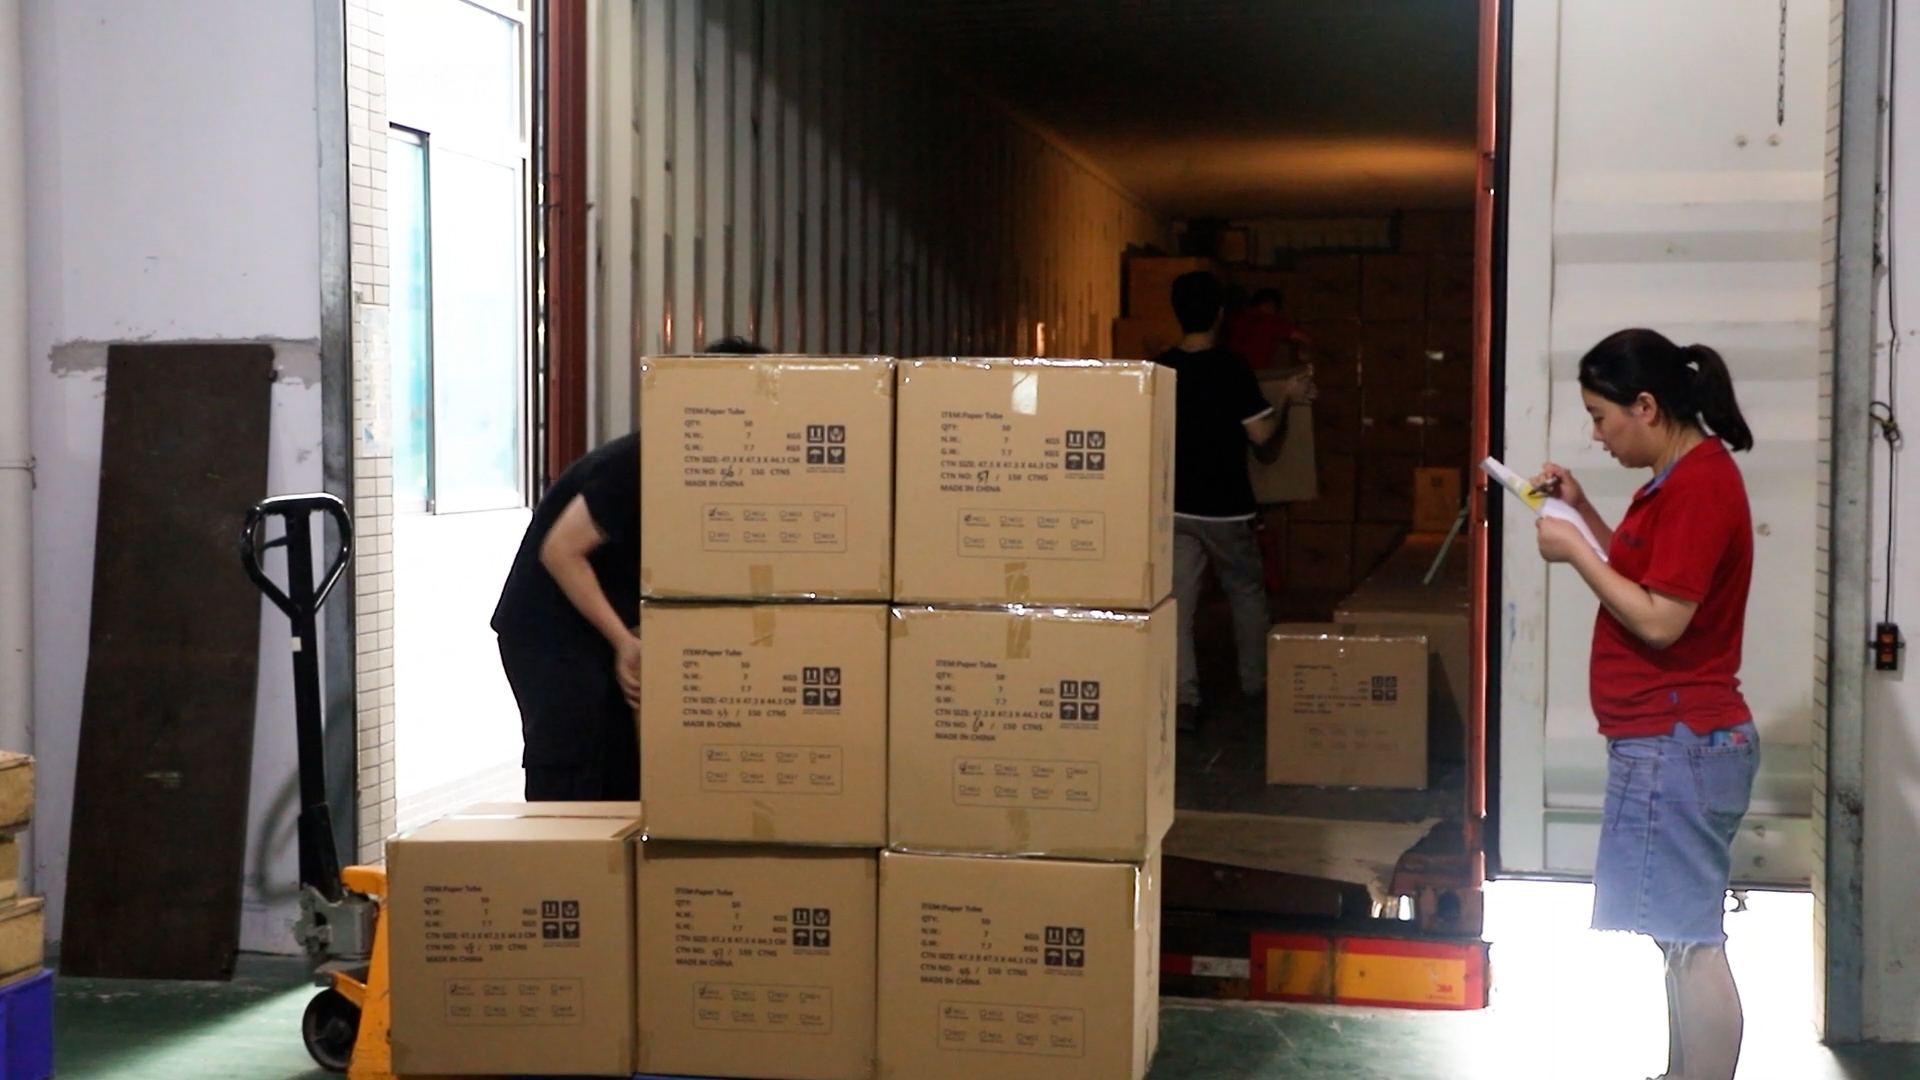
Founder Matt insists that customer trust is the cornerstone of corporate development. We implement a "VVIP service system" regardless of order size, providing 1-on-1 dedicated account managers, 24/7 customer support, real-time production progress tracking, and rapid after-sales response. Leveraging the industrial cluster advantage, we ensure a stable supply of raw materials and efficient logistics arrangements for sea and air freight to New Zealand ports, achieving an on-time delivery rate of over 98% and a customer repurchase rate of over 85%. Our professional team offers packaging structure optimization, cost control suggestions, and compliance guidance.
With years of experience in serving international brands, CZY has won wide recognition from clients in Europe, North America, Southeast Asia, and Oceania, particularly in New Zealand. We do not only manufacture packaging products but also engineer tailored solutions using AI and advanced mechanics to help brands stand out in the market. We cherish every order and strive to build long-term, win-win business partnerships with global clients through premium quality, professional service, and competitive costs. CZY is your reliable partner for high-end airplane paper box and tube packaging, accompanying your brand to global success.
Explore our full range of customizable, eco-friendly packaging solutions. Whether you are shipping high-end cosmetics from Auckland or artisanal essential oils from Rotorua, our meticulously crafted paper tubes and boxes ensure your product arrives beautifully and sustainably.